
Metal Parts Manufacturer Quality Control
| Link | What is recorded | Why it matters |
|---|---|---|
| Raw material | Source, usage, heat number | Confirms the alloy is what you ordered |
| Process | Parameters, speeds, feeds | Shows the part was made to plan |
| Machine | Running data, batch | Locates the equipment for a drift |
| Operator | Who ran the job, when | Completes the accountability chain |
| Inspection | CMM, SPC results | Proves the part measured right |
Which certifications back the quality system?
| Standard | Certificate number | Scope |
|---|---|---|
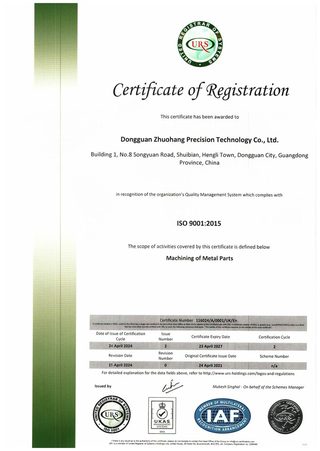
| ISO 9001:2015 | 116024/A/0001/UK/En | Machining of metal parts |
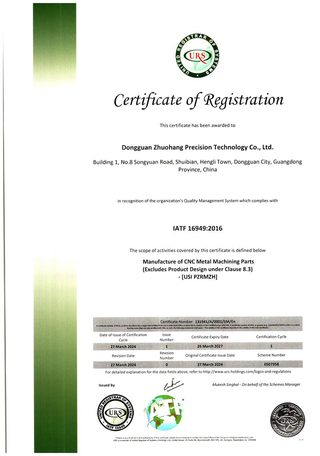
| IATF 16949:2016 | 131941/A/0001/SM/En | Manufacture of CNC metal machining parts (excludes product design, Clause 8.3) |
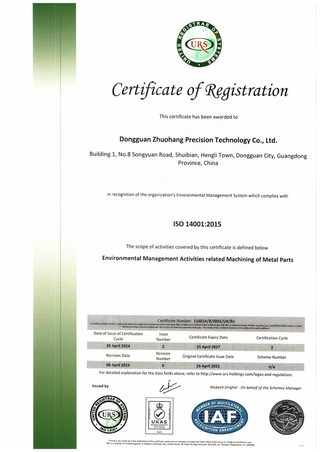
| ISO 14001:2015 | 116024/B/0001/UK/En | Environmental management related to machining of metal parts |
Honest scope note: IATF 16949 excludes product design under Clause 8.3. We are a build-to-print manufacturer — you own the design, and we own making it repeatably to your print, with the records to prove it.
What process capability does the shop prove?
A capability statement is worthless without a control chart. On a representative length characteristic (76.1–76.5 mm), our SPC shows Cpk 1.851 (one characteristic on one part, not a blanket capability claim) against an initial-study target of Ppk ≥ 1.67, with general characteristics held to Cpk ≥ 1.33. The chart is part of the traceability record.
A single Cpk number out of context means little. What matters is the control chart behind it: a process that is stable and centered between its limits, sampled over time, not a one-off measurement. When a supplier quotes Cpk, ask to see the chart. A number without a chart is a claim; a chart is the process talking.
| Characteristic class | Target | Evidence to ask for |
|---|---|---|
| Key characteristic | Ppk ≥ 1.67 initial | Control chart on the named dimension |
| General characteristic | Cpk ≥ 1.33 | Same chart, wider band |
| Verified dimension | In tolerance | Per-lot CMM report, shipped with parts |
How is a part inspected before it ships?
The inspection bench closes the chain with proof, and the results are documented.
- Hexagon GLOBAL S CMMs (2) for dimensional verification, plus a gear measuring center and vision measuring machines.
- KEYENCE VK-X3000 laser microscope and SURFCOM 1800D for surface finish and profile.
- XRF (iCHEQ) spectrometer for incoming material composition checks.
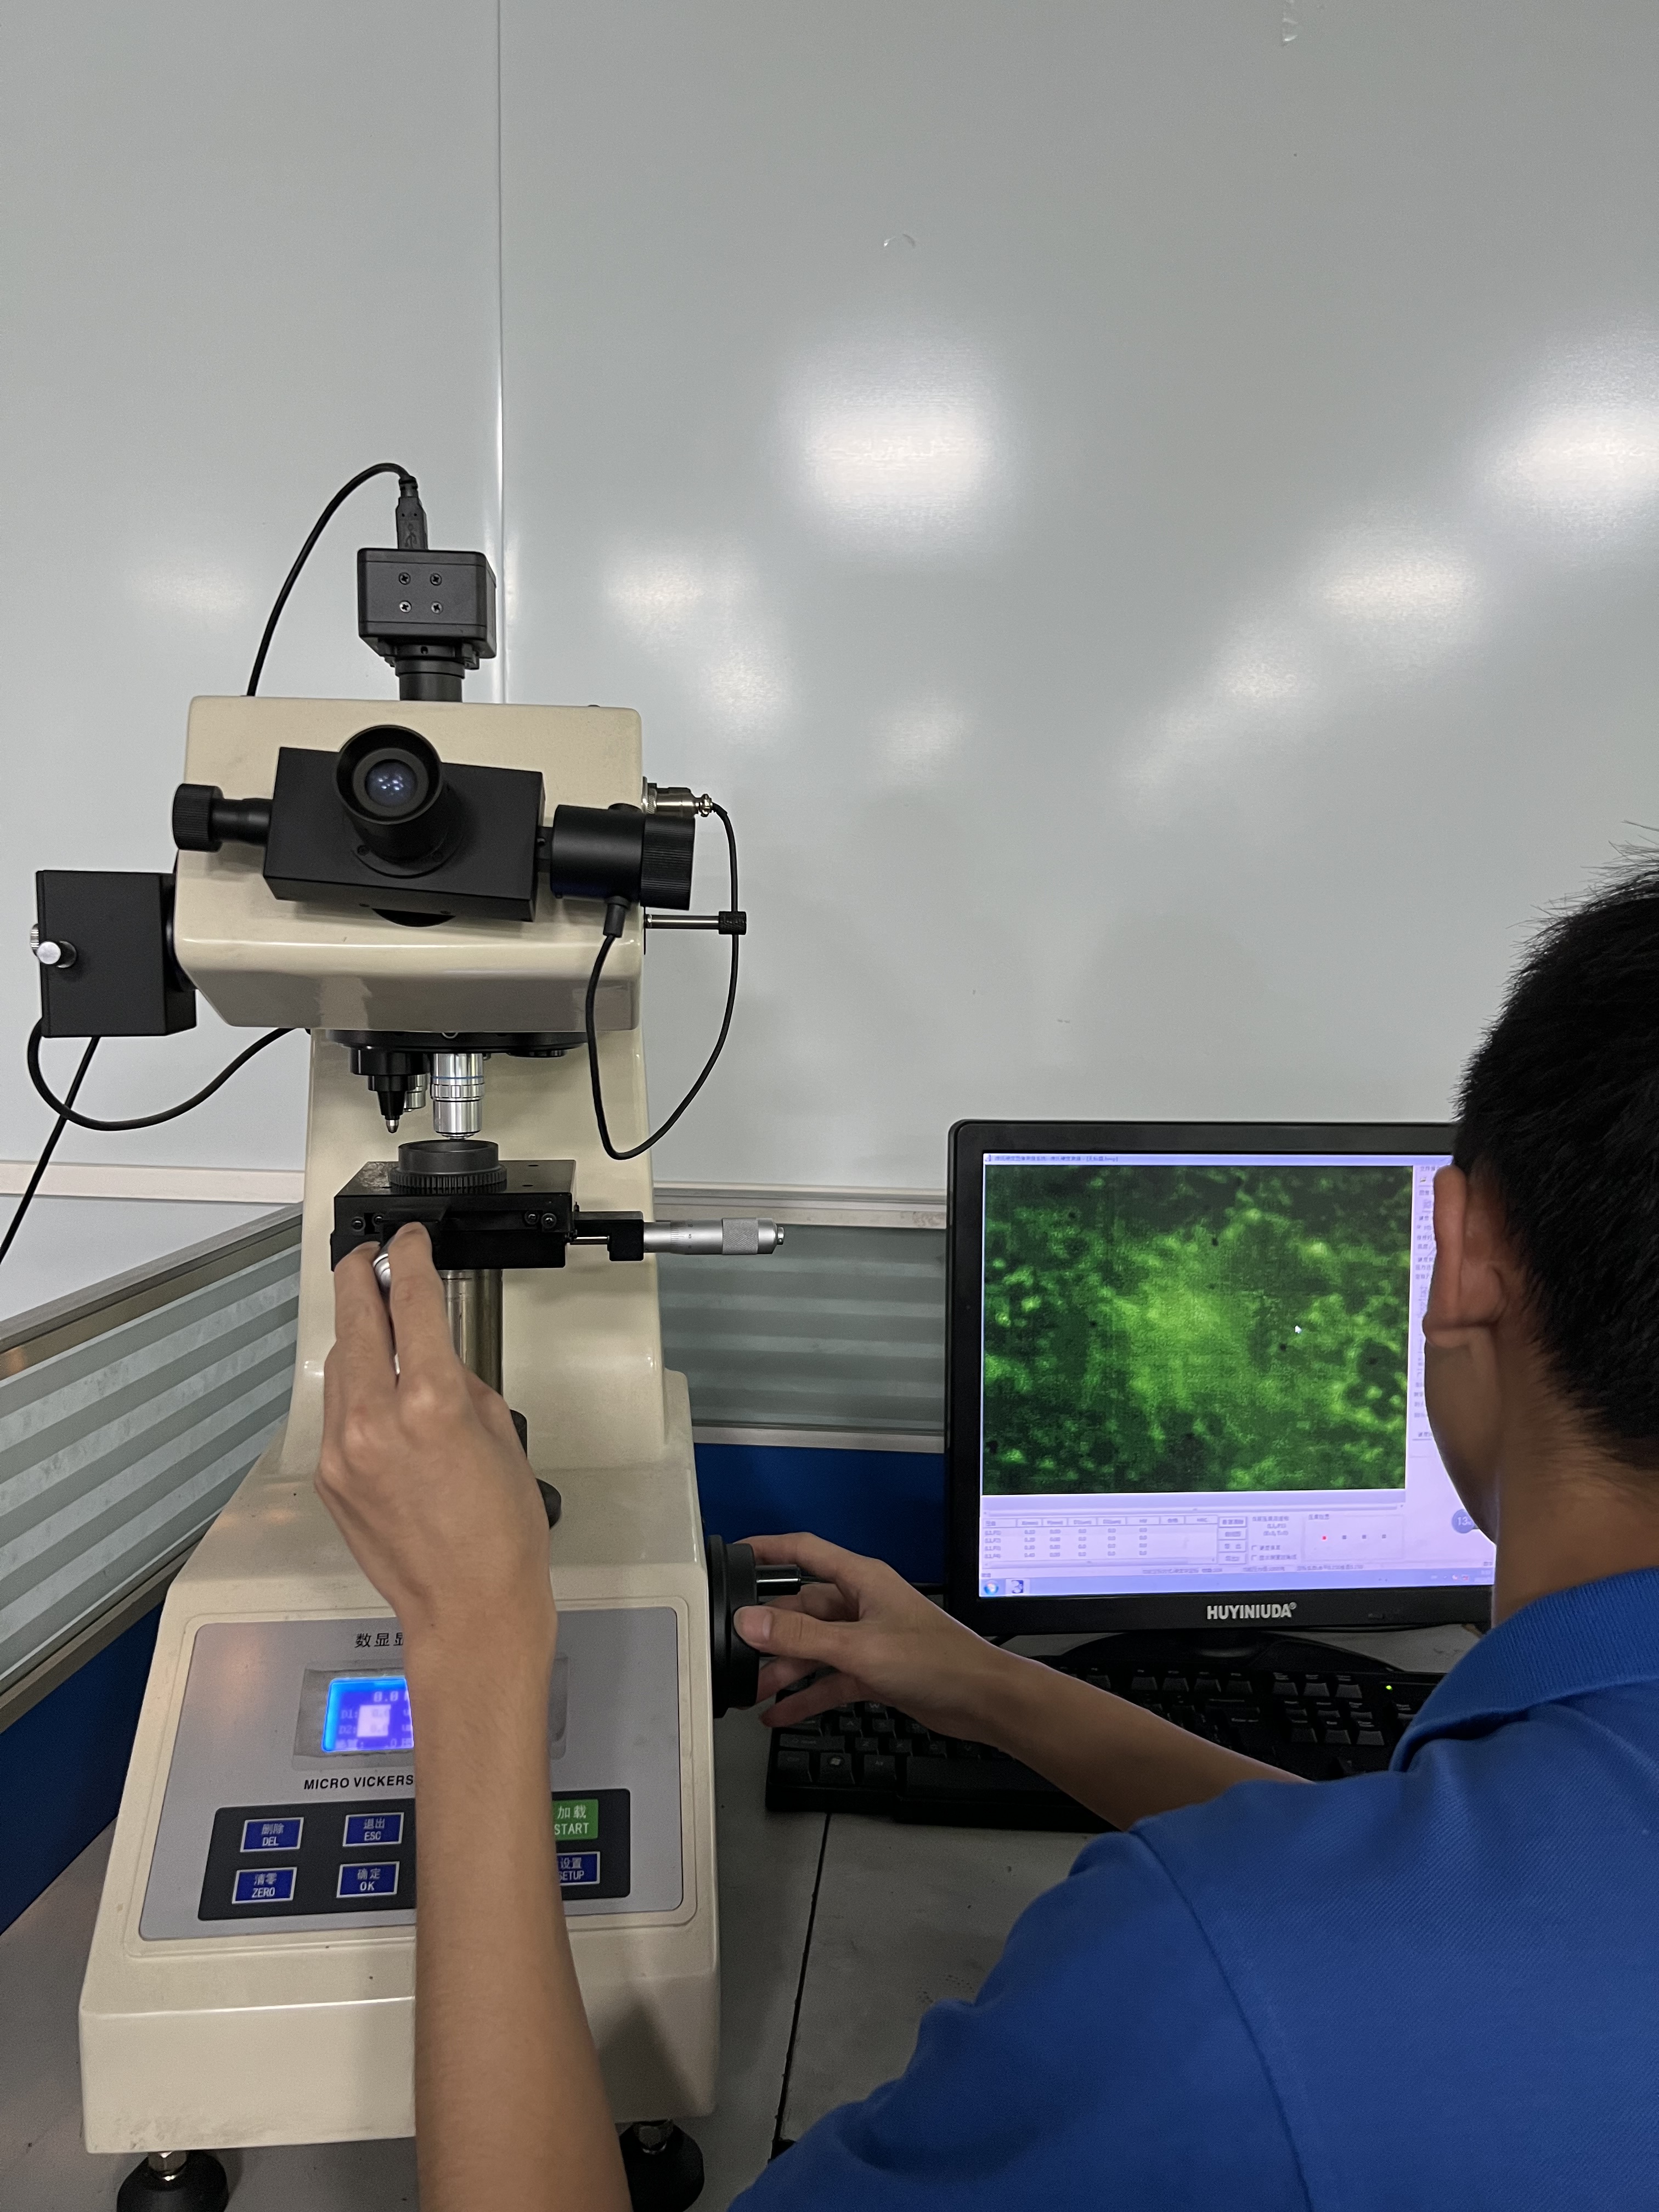
- HVS-1000A micro-Vickers hardness tester, Fischer coating gauge, salt spray and tensile testers.
How does traceability support a recall or containment?

If a non-conformance surfaces, the chain tells you which lot, which machine, and which operator is involved. You recall the affected lot, not the whole shipment. That is the difference between a contained defect and a product recall, and it is why automotive buyers demand the chain before they order.
Containment is cheaper than recall because the boundary is drawn by the record, not by the shipping date. Without a batch record, the only safe answer is to hold every part from that week. With one, the hold stops at the affected lot and the rest keeps moving.
Can the shop provide a PPAP package?
For automotive and regulated buyers, a PPAP package proves the process is under control. Our APQP/PPAP evidence includes process flow charts, control plans, SPC charts, and PFMEA — all traceable to the lot, and all part of the same quality record.
How do you verify the quality claims before you buy?
Every claim on this page can be checked. Ask for the evidence and compare it to what you were told.
- Ask for the certificate numbers, then confirm the scope with the registrar — a number without a verifiable scope is decoration.
- Ask for a Cpk chart on a real dimension, not a summary sentence.
- Ask what ships with a lot. CMM reports, SPC charts, and a material certificate are the record; a pass/fail sticker is not.
- Ask whether the IATF scope excludes design. A build-to-print shop that says so is being honest about what it controls.
How is Cpk read correctly?
Cpk is a process capability index that compares the spread of a process against its tolerance limits. A Cpk of 1.0 means the process just fits the tolerance; a Cpk of 1.67 means the process has enough room that a small drift will not produce a bad part. The number only means something when it is read against its chart, because a single Cpk without the underlying data is a claim, not a measurement.
Two things make a Cpk trustworthy. First, the sample has to be spread over time — a capability number computed from parts made in one hour says nothing about next week. Second, the process has to be stable — a control chart with points jumping around inflates the spread and deflates the Cpk. When a supplier quotes Cpk, ask for the chart. A number without a chart is a story; the chart is the process talking, and it is the chart that closes the loop.
| Characteristic class | Target | Evidence to ask for |
|---|---|---|
| Key characteristic | Ppk ≥ 1.67 initial | Control chart on the named dimension |
| General characteristic | Cpk ≥ 1.33 | Same chart, wider band |
| Verified dimension | In tolerance | Per-lot CMM report, shipped with parts |
How does SPC turn a measurement into a prediction?
Statistical process control turns a stream of measurements into an early warning. Instead of asking "is this part in spec," the control chart asks "is the process drifting toward the edge." A chart that trends steadily toward a limit catches the drift while the parts are still good, so the correction happens before scrap exists. That is the difference between a quality system that reacts to bad parts and one that sees the bad part coming.
The chart is also part of the traceability record, because it ties the process behavior to the lot. When a non-conformance surfaces, the SPC chart shows whether the drift was sudden or gradual, which points to the cause — a broken tool, a changed offset, a worn insert. A shop that keeps SPC charts has the root cause already half-found; a shop that does not is starting the investigation from zero. That is why the chart is filed against the lot, not kept as a summary.
What is a measurement system analysis?
Measurement system analysis — often run as a gauge repeatability and reproducibility study, or GR&R — checks whether the measuring instruments can actually tell good parts from bad. A caliper held by two operators can give two different answers, and if that variation is a large slice of the tolerance, the measurements are noise. The study quantifies that noise before the measurements are trusted, and it is run before the instruments are relied on in production.
The reason it matters to the chain is simple: the chain's last link is measurement, and a measurement you cannot trust is a link that does not close. A shop that runs a GR&R on its CMMs and profilometers has verified that the numbers on the report mean what they say. A shop that skips it is writing numbers it has not proven it can produce. When you audit a quality system, ask how the measurement system was validated, not just what the instruments are. The answer separates a shop that measures from one that only records.
How do PPAP levels change the package?
The production part approval process has levels that decide how much evidence ships with a submission. At the lowest level, the supplier holds the records and submits a warrant; at higher levels, the dimensional results, material certs, and capability studies are submitted with the parts. The level is a contract about how much proof you receive, and it is set by your risk, not by convenience.
The package itself is what matters: process flow charts, control plans, SPC charts, and PFMEA, all traceable to the lot. Those four documents are the traceability chain written in the formal language an automotive auditor checks, and they are the same documents a non-automotive buyer can lean on for the same confidence. A PPAP is not extra paperwork; it is the chain, formatted for submission. Because the shop runs IATF 16949-grade discipline on every job, the underlying documents are already being written — the PPAP simply assembles them into the submission a program requires.
How does calibration keep the record trustworthy?
An instrument that drifts writes a record that lies. A CMM out of calibration reads a part in spec when it is out, or out when it is in, and either error is a cost. Calibration is the schedule that keeps the measuring instruments honest, and the calibration records are part of the chain, because they prove the numbers on the report were produced by instruments that were themselves verified.
The same logic extends to the process: the SPC charts, the CMM reports, and the material certificates are only as reliable as the instruments behind them. A quality system that tracks calibration is a system whose measurements you can trust without re-checking every box. Ask when the CMMs and profilometers were last calibrated, and the answer tells you whether the record is built on verified instruments or on assumption.
Calibration is also what makes a comparison between suppliers possible. Two shops can both say they hold ±0.003 mm (milling) / ±0.002 mm (turning), but only the one with a calibration schedule and a GR&R on record can prove the number means the same thing on its floor as it does on yours. The record is only as strong as the instruments that wrote it, and calibration is the discipline that keeps those instruments honest.
The inspection bench here is the same class of equipment a buyer would use to audit the factory, and it is held to the same calibration discipline: Hexagon GLOBAL S CMMs for dimensional verification, a KEYENCE VK-X3000 laser microscope and a SURFCOM 1800D for surface finish and profile, an XRF spectrometer for material composition, and hardness, coating-thickness, salt-spray, and tensile testers for the physical properties. Each instrument writes a record, and the calibration schedule is what keeps every one of those records honest.
What this shop actually runs
Ask for capability evidence and the answer should be specific. The facility behind this guide runs 100+ CNC machines on a 6,800 m2 floor in Dongguan, China, with 100+ staff. The machine list, by category:
- 5-axis machining centres (10+) - Mazak VARIAXIS I-600 (510/910/510 mm travel, 12,000 rpm, 22 kW, 71.6 N·m, 30-tool BT40) and Mazak INTEGREX I-250H S (B-axis 0.0001°, 24 kW, 124 N·m, 38-tool HSK-A63). Used for compound-angle parts, single-setup multi-face prismatic work, and aerospace fittings where datum transfer loss is unacceptable.
- 3-axis / 4-axis machining centres (50+) - Brother SPEEDIO S500Z2N / S700Z2N (10,000 rpm, 14/21-tool ATC, 0.7 s tool-to-tool, Z-axis 2.2 G) and Mazak VCE-430A L / VCE-570C L (10,000 rpm, 118 N·m, 24-tool ATC). Used for prismatic parts, plates, brackets, housings.
- Swiss-type turning centres (10+) - Citizen Cincom A20-3F7 (Φ20 mm, 10,000 rpm), TSUGAMI B0206-III / B0205-III (Φ20 mm, 0.1 µm), STAR SR-32JII / SR-32J Type N (Φ32 mm, 8,000 rpm). Used for long, slender rotational parts at ±0.002 mm.
- CNC turning centres (20+) - HEADMAN T70M/1250 (720 mm swing, 117 mm bore, 3,000 rpm, BMT75 12-station turret). Used for shafts, bushings, flanges up to ±0.002 mm.
- Wire EDM (5+) - Sodick AQ535L (550/350/300 mm travel, ±20° taper, 800 kg workpiece). Used for hardened tool steel, internal splines, sharp internal corners that milling cannot reach.
- Inspection: Hexagon CMM + 20+ gauges - Hexagon CMM for coordinate measurement, plus vision system, profilometer, hardness tester, coating thickness gauge, XRF for material verification. The 10:1 rule (gauge 10x more accurate than the band) is applied to every feature.
- Machine highlights - VARIAXIS I-600: one-setup multi-face 5-axis + MAZA-CHECK auto-calibration; INTEGREX I-250H S: DONE-IN-ONE mill-turn, B-axis 0.0001° + Ai thermal shield; SPEEDIO S500Z2N / S700Z2N: Z-axis 2.2 G + 0.7 s ATC; Swiss-type: guide-bush switchable + 0.1 µm resolution.
Tolerances held: milling ±0.003 mm, turning ±0.002 mm, grinding and wire EDM ±0.002 mm. Capability: Ppk >= 1.67 initial and Cpk >= 1.33 in production on key characteristics.
Certifications: ISO 9001:2015 (116024/A/0001/UK/En), IATF 16949:2016 (131941/A/0001/SM/En, clause 8.3 design excluded, disclosed openly) and ISO 14001:2015 (116024/B/0001/UK/En), issued to Dongguan Zhuohang Ltd, USCC 91441900MA4UWT6X39, established 2005.
Service area: Austria, Belgium, the Czech Republic, Denmark, France, Germany, Greece, Hungary, Ireland, Italy, the Netherlands, Spain, Sweden and the United Kingdom in Europe; Brazil, Canada, Mexico and the United States in the Americas; China, Israel, Japan, Singapore and Sri Lanka in Asia; Australia and New Zealand in Oceania; and South Africa in Africa — built in China, shipped worldwide.
Contact: Felipe Iglesias, [email protected], +86 13126536955.
Verify the traceability chain yourself
Email [email protected] or call +86 13126536955 and ask for the certificate numbers, a Cpk chart, and a material certificate.
Frequently Asked Questions
How does traceability define the quality system?
In short, Quality is the ability to prove what happened on every lot. MES/ERP records material source and usage, process parameters, machine data, batch, machining time, operator, and inspection results, so a defect is traced to its root in minutes rather than left a mystery.
Which certifications back the quality system?
ISO 9001:2015 (No. 116024/A/0001/UK/En), IATF 16949:2016 (No. 131941/A/0001/SM/En), and ISO 14001:2015 (No. 116024/B/0001/UK/En). The IATF 16949 scope excludes product design under Clause 8.3.
What process capability does the shop demonstrate?
In short, On a representative length characteristic (76.1–76.5 mm), the SPC shows Cpk 1.851 (one characteristic on one part, not a blanket capability claim) against an initial-study target of Ppk ≥ 1.67, with general characteristics held to Cpk ≥ 1.33. Read the tolerance band before you read the index.
How are parts inspected before they ship?
Critical dimensions are verified on Hexagon GLOBAL S CMMs, supported by a KEYENCE VK-X3000 laser microscope, a SURFCOM 1800D for surface finish, an XRF spectrometer for material, and hardness, coating-thickness, salt-spray, and tensile testers.
Can the shop provide PPAP and control plans?
Yes. The automotive-grade APQP/PPAP package is supported by process flow charts, control plans, SPC charts, and PFMEA, reflecting the IATF 16949 build-to-print discipline.
Metal Parts Manufacturer Quality — Related Pages
Standards referenced on this page
- IATF 16949:2016 — Automotive quality management system standard
- ASTM A582/A582M-12 — Standard Specification for Free-Machining Stainless Steel Bars
- ISO 14001 — Environmental management systems — Requirements with guidance for use